


China Testing & Certification International Group Co., Ltd. (CTC, Stock Code 603060) originated from the testing and certification business of China Building Materials Academy in the 1950s. After 70 years of unremitting efforts and persistent pursuit, the company has formed five business categories: detection and testing, certification and evaluation, testing instruments and intelligent manufacturing, measurement and calibration, scientific research and technical services, committed to providing customers with technical services and comprehensive solutions of detection and testing, certification and evaluation, appraisal, consultation, training, and instruments and equipment in fields of quality, environmental protection, green, safety, health, and energy conservation.
- Detection and Testing
- Certification and Evaluation
- Testing Instruments and Intelligent Manufacturing
- Measurement and Calibration
- Scientific Research and Technical Service
- Aerospace
- Automobile and Parts
- Intelligent Manufacturing
- Rail Traffic
- Photovoltaic
- Wind Power
- Electrical Engineering
- Building Materials and Construction Engineering
- Cement and Cement Products
- Glass
- Water Resources
- Special Equipment
- Geology and Mineral Resources
- Low-carbon Environmental Protection and Green Certification
- Environment and Safety
- Cosmetics and Daily Chemicals
- Food and Agricultural Products
- Digital Services
- International Business
- New Materials Testing
- Fiber Reinforced Plastics Product Testing(Composite Materials Testing)
- Friction Material Testing
- Non-metallic Sealing Products Testing
- Building Materials Testing
- Decoration Materials Testing
- Cement and Primary Combustion Materials Testing
- Glass Materials Testing
- Building and Sanitary Ceramics Testing
- Stone Testing
- Refractory Materials Testing
- Waterproof and Water-saving Materials Testing
- Fiberglass Product Testing
- Engineering Materials Testing
- Cement Concrete Product Testing
- Green Wall Materials Testing
- Mineral Products Testing (Metallic and Non-Metallic)
- Photovoltaic Products Testing
- Wind Turbine Blade Testing
- Coal Testing
- Power Testing
- Chemical Product Testing
- Textile Testing
- Special Equipment Testing
- Construction Engineering Testing
- Highway Engineering Testing
- Civil Air Defense Engineering Testing
- Water Conservancy Project Testing
- Nuclear Power Engineering Testing
- Indoor Environment Testing
- Detection Business
- Ecological Environment, Health and Safety Testing
- Food Safety and Agricultural Consulting
- Our Services
- Information Disclosure
- Certificate Inquiry
- Online Application
- Application Documents Download
- Intelligent Instrumentation
- Equipment R&D and Manufacturing
- Operation and Maintenance of Environmental Monitoring Equipment
- Building Engineering Forensic Appraisal
- Product Quality Forensic Appraisal
- Environmental Damage Forensic Appraisal
- Public Security Drug Testing
- Smart Water Conservancy
- Smart Agriculture
- Smart Environmental Protection
- Safety Technical Services
- Environmental Protection Technology Services
- Operation and Maintenance of Environmental Monitoring Equipment
- Ecological Environment Consulting
- Project and Fund Application
- Education and Training
- Informatization and Intelligent Construction of Safety Production
- Energy Efficiency Evaluation
- Fire Safety Field
- Laboratory Construction Services
- Quality Improvement Service
- Research Services
- Room Temperature Static Mechanical Performance Testing...
- Room Temperature Dynamic / Long-Term Mechanical Performance Testing...
- Thermal Performance Testing
Optical Performance Testing Electrical Performance Testing - Extreme Environment Testing of Static Mechanical Properties at Low, High and Ultra-High Temperatures...
- Low, High and Ultra-High Temperature Dynamic / Long-Term Mechanical Performance Testing...
- Thermal Shock Resistance Testing of Materials
- Oxidation Resistance Evaluation of Materials
- Jacking Pipe Testing
- Pressure Pipe Testing
- Open-Circuit Cooling Tower Testing
- Closed-Circuit Cooling Tower Testing
- FRP Chimney Inner Liner / Flue Duct Testing
- Septic Tank Testing
Septic Tank Testing - Cable Bracket (Cable Support) Testing
- Grille (Grating) Testing
- Structural Profile Testing
- Buried Double-Wall Oil Tank Testing
- Corrosion-resistant Storage Tank Testing
- Corrugated Panel Testing
- Unit Bathroom Testing
- Automobile Brake Lining Testing
Clutch Facing Testing Testing of Brake Pads/ Bands for Various Industrial and Agricultural Machinery... - Brake Pads for Motorcycles and Mopeds Testing
Automotive Clutch Assembly Testing Automobile Brake Assembly Testing - Oil Drilling Rig Brake Block Testing
- Elevator Brake Friction Block Testing
Drilling Brake Pad Testing - Brake Pads for High-speed Rail and Subway Testing
- Wind Turbines Brake Pads for the Main Shaft and Yaw Brake Testing...
Testing of Sheet Material for Non-metallic Sealing Gaskets... Testing of Non-metallic Sealing Gasket and Its Composite Reinforced Gasket... Geology and Mineral Resources Testing of Non-metallic Materials for Dynamic Sealing... Packing Filler Testing Internal Combustion Engine Cylinder Head Gasket Testing... Winding Gasket Testing
Building Materials and Construction Engineering Geosynthetic Materials Testing Waterproof Material Testing Reinforcement Material Testing Concrete Testing Wire and Cable Testing Ventilation Duct Testing Seismic Bracing and Suspension Testing
- Paint and Coating Testing
Adhesive Testing Dry-mixed Mortar Testing Waterproof and Sealing Materials Testing - Natural and Artificial Stone Materials Testing
Ceramic Tile Testing Sanitary Ware Testing Faucet Valve Testing Pipes and Fittings Testing Fresh Air System Testing Gypsum Board Testing Sunshade Products Testing Floor Testing Negative Ion Products Testing Sanitary and Kitchen Furnishings Testing Metal Decorative Materials Testing Sports Venues and Flooring Materials Testing
Primary Combustion Materials Testing Clinker Testing Special Cement Testing Ordinary Portland Cement Testing Mixed Material Testing Packaging Bag Testing Grinding Aid Testing Comparative Verification Testing, Type Testing, Production License Testing, Voluntary Product Certif... Performance Testing of Co-processing Products in Cement Kilns...
Quartz Glass Testing Locomotive and Aircraft Glass Automotive Paint Protection Film and Window Film Building, Automotive, Electronic, and Smart Glass Equipment and Testing Technology Development
Ceramic Tile Testing Sintered Stone Testing Building Materials and Construction Engineering Architectural Glazed Products Testing Anti-static Porcelain Flooring Testing Glass Mosaic Testing Architectural Decorative Microcrystalline Glass Testing... Microcrystalline Glass Composite Board Testing Permeable Brick Testing Plaza Brick Testing Dry-hanging Hollow Ceramic Panel Testing Bathroom Products Testing Building Materials and Construction Engineering Smart Bathroom Testing
- Natural and Artificial Stone Materials Testing
Dense Shaped Refractory Products Testing Monolithic Refractory Material Testing Insulating Refractory Products Testing
Waterproof Roll Material Testing Waterproof Coating Testing Leakage Stoppage and Grouting Material Testing Sealing and Adhesive Material Testing Geosynthetic Material Testing Testing of Tile Adhesive Series Materials Building Anchor Bolt/ Fastener Testing
Glass Wool Testing Rock Wool Testing Foam Plastic Testing Foam Glass Testing Aerogel Testing Vacuum Insulation Panel Testing Testing of Various Inorganic/ Organic Insulation Materials... Glass Fiber Testing Basalt Fiber Testing Carbon Fiber Testing High-performance Fiber and Product Testing Fiber-reinforced Composite Material Testing
Concrete and Constituent Materials Testing Waterproof Material Testing Thermal Insulation Material Testing Metal Material Testing Mortar Testing Cable Testing Doors, Windows and Curtain Walls Testing Heating and Heating Equipment (heating radiators, etc.) Testing...
Electric Pole Product Testing Testing of Ultra-high Performance Concrete Utility Pole Products... Testing of Electric Power Steel Pipe Poles Testing of Other Electric Power Products Power Cover Plate Testing Cable Trench Testing Box-type Substation Testing Testing of Ring Main Unit Foundation (MPP、CPVC、UPVC) Testing of Conduits for Power Cables in Electric Power Ducts (MPP, CPVC, UPVC)... Raw Material Testing for Poles
Sintered Bricks and Blocks Testing Non-sintered Bricks and Blocks Testing Wall Panel Testing Concrete Tile Testing Concrete Paving Tile Testing Concrete Curb Testing Permeable Pavement Tiles and Permeable Pavement Slabs Testing... Tactile Guide Path Tiles Testing
Graphite Testing Fluorite Testing Talc Testing Pyrophyllite Testing Gypsum Testing Barite Testing Magnesite Testing Calcium Carbonate Testing Quartzite Testing Marble Testing Granite Testing Kaolin Testing Bentonite Testing Attapulgite Testing Diatomaceous Earth Testing Sepiolite Testing Mica Testing Chrysotile Asbestos Testing Vermiculite Testing Cosmetics and Raw Material Testing Feldspar Testing Clay Testing Quartz Stone (Sand) Testing Silicate Testing
Outdoor Empirical Testing of Photovoltaic Modules Photovoltaic Module/ Component/ Material Testing Photovoltaic Power Station Grid-connected Photovoltaic Inverter Testing
Full-size Wind Turbine Blade Testing
Electric Power Tools and Equipment Testing
Inorganic Industrial Product Testing Lithium Battery Cathode Materials and Precursors Testing... Water Treatment Agent Testing Basic Organic Raw Material Testing Synthetic Polymer Material Testing Organic Fine Chemical Product Testing
- Daily Textile Testing
Non-destructive Testing of Metallic Materials Regular Detection of Pressure Pipelines Regular Detection of Pressure Vessels
Testing of Building Materials and Components Testing of Main Structure and Decoration Steel Structure Testing Foundation Testing Building Energy Efficiency Testing Building Curtain Wall Testing Municipal Engineering Material Testing Road Engineering Testing Bridge and Underground Engineering Testing Lightning Protection Testing Foundation Pit Monitoring
Highway Engineering Material Testing Subgrade and Pavement Testing Concrete Structure Testing Foundation Pit and Foundation Pile Testing Traffic Safety Facility Testing Third-party Central Laboratory Testing Handover and Completion Acceptance Bridge and Tunnel Testing
Factory Quality Testing of Protective Equipment Products for Civil Air Defense Projects... Process Control and Installation Quality Testing of Protective Equipment for Civil Air Defense Proje... Completion Acceptance and Installation Quality Testing of Protective Equipment for Civil Air Defense...
Concrete Engineering Testing Geotechnical Engineering Testing Measurement Metal Structure Testing Mechanical and Electrical Testing
Dry-mixed Mortar Testing Comprehensive Performance Testing of Concrete Aggregate Testing Insulation Board Testing
- Limit Testing of Harmful Substances
Hazardous Substance Emission Testing Evaluation of Biodegradability of Building Materials... Health and Safety Testing Solid Waste Testing Mildew and Antibacterial Testing Material Analysis and Failure Diagnosis Odor Evaluation Environmental Control
Detection of Tempered Glass Homogenization Furnace Detection of Photovoltaic Systems and Key Components... Detection of Cement, Lime, Gypsum and Their Products... Detection of Architectural Decoration and Finishing... Building Structure Detection - Building Curtain Wall Detection
Water Quality Testing Gas Testing Solid Testing Noise Testing Ecological Testing Food Quality and Safety Testing Agricultural Quality and Safety Testing Specialized Testing of Traditional Chinese Medicinal Materials... Radiation Testing New Pollutant Testing
- Investigation of Safety Risks and Hidden Dangers in Food Enterprises...
Farmland Quality Survey and Grade Evaluation Restoration and Management of Farmland with Production Obstacles... Technical Services for Pilot Projects of Green Planting and Breeding Circular Agriculture... Acidic Soil Remediation Investigation into the Genesis and Source of Heavy Metals...
- Safety Glass CCC Certification
Ceramic Tile Certification - Automobile Brake Linings Certification
Green Product Certification - Green Building Materials Products Certification
Low-carbon Product Certification - Child-Friendly Product Certification
- Product Health Performance Certification
- Age-Friendly Product Certification
- Near-zero Energy Buildings Products Certification
Quality Management System Certification Environmental Management System Certification Occupational Health and Safety Management System Certification... Energy Management System Certification - Healthy Space Creation Services Certification
- Testing and Evaluation Services Certification
- Engineering Cost Consulting Services Certification
- Construction and Installation Services Certification in Building Engineering...
Carbon Footprint Certification - Greenhouse Gas Management System
Low-carbon Product Certification ISCC International Sustainability and Carbon Certification... - CDM Validation and Certification
- RSB Certification
- VCS Project Validation and Verification
- CCB (Climate Community and Biodiversity)
CBAM Consultation ISO14064 EPD Service Carbon Footprint Service - Green Manufacturing System Service
Clean Production Audit Consultation on Pollutant Discharge Permit Environmental Compliance Assessment Environmental/ Safety Emergency Response Plan Ultra-low Emission Consultation and Evaluation Energy Audit Energy-saving Diagnosis Energy Conservation Supervision Energy Saving Audit
Laboratory High-end Equipment Manufacturing and Automation System Integration... Comprehensive Intelligent Operation and Maintenance of Laboratory Equipment...
Environmental Protection and Safety Equipment
Construction, Operation and Maintenance of Automatic Air and Water Quality Monitoring Stations... - Construction, Operation and Maintenance of Automatic Monitoring Facilities for Key Polluting Enterpr...
Perchlorate Online Monitoring and Perchlorate Wastewater Treatment Equipment...
Calibration of Geometric Quantity (Length) Mechanical Calibration Thermology Calibration Acoustic Calibration Electromagnetic Calibration Radio Calibration Time and Frequency Calibration Optical Calibration Chemical Calibration Calibration of Specialized Measuring Instruments for Textiles and Leather... Calibration of Specialized Measuring Instruments for Motor Vehicles... Calibration of Specialized Measuring Instruments for Meteorology and Oceanography... Calibration of Specialized Measuring Instruments for Paper Making and Paper Products... Calibration of Medical-specific Measuring Instruments... Calibration of Specialized Measuring Instruments for Chemical Industry... Calibration of Specialized Measuring Instruments for Construction and Transportation... Calibration of Specialized Measuring Instruments for Electrical Engineering, Electronics and Electri... Medical Device Testing Electrical Testing Metrology and Standard-setting Technical Services
Engineering Testing Quality Appraisal Quality Appraisal of Municipal Engineering Projects...
Appraisal of Graphite and Other Non-metallic Materials... Appraisal of Glass and Glass Products Photovoltaic and Solar Thermal Device Appraisal Plaster Appraisal Appraisal of Cement and Its Products Brick and Tile Appraisal Appraisal of Stone Building Materials Ceramic Product Appraisal Refractory Material Appraisal Appraisal of Safe Metal Products Appraisal of Metal Surface Coatings
Environmental Damage Forensic Appraisal
Hair Drug Testing Sewage-based Drug Testing
Rainwater Monitoring & Reporting and Dam Safety Early Warning System for Small-medium Reservoirs... Smart Inspection System for Reservoir Property Management... Smart Irrigation District Management Platform Happiness River and Lake Management Platform
Farmland Environment Automatic Monitoring System Intelligent Integrated Irrigation and Fertilization Control System... Intelligent Valve Automatic Irrigation Control System... Intelligent Greenhouse Control System Intelligent Aquaculture System
- Digital Management Platform for River Discharge Outlets and Key River Basin Water Environment...
Standardization Construction of Safety Production Safety and Environmental Protection Audit On-site Hidden Danger Inspection Safety and Environmental Protection Due Diligence Safety and Environmental Protection Training
Environmental Impact Assessment Environmental Management Environmental Acceptance Pollutant Discharge Permit Ultra-low Emission Service Cement Kiln Co-processing Performance Test
Construction, Operation and Maintenance of Automatic Air and Water Quality Monitoring Stations... Construction, Operation and Maintenance of Automatic Monitoring Facilities for Key Polluting Enterpr... Perchlorate Online Monitoring and Perchlorate Wastewater Treatment Equipment...
Soil Pollution Survey Hazardous Waste Identification Customized Services for Key Soil Pollution Supervision Units... Pre-assessment and Assessment Monitoring of Ultra-low Emissions... Performance Grading for Heavy Pollution Weather Environmental Protection Acceptance Inspection upon Completion of Construction Projects... Park Environmental Management Emergency Response Plan for Sudden Environmental Incidents... Declaration of Enterprise Pollutant Discharge Permit and Post-permit Management...
Planning and Application of Central Budgetary Investment and Ultra-long-term Treasury Bond Projects... Application for Funds Deposited into the Ministry of Ecology and Environment's Account...
Training on Safety Production Knowledge and Management Ability for Main Responsible Persons and Safe... Pre-examination Training for Intermediate Certified Safety Engineer... Continuing Education for Intermediate Certified Safety Engineers... Enterprise Safety and Occupational Health Compliance Training...
Standard Interpretation Planning and Design Furniture Configuration Instrument Selection CMA and CNAS Certification Consulting Testing Equipment R&D Laboratory Instrument and Equipment Automation Upgrade Service... Building a Digital Quality Management Platform for Laboratories... Supply of Chemical Reagents and Consumables
Advanced Quality Control Technology Services Equipment R&D and Sales RM/Standard Samples R&D and Sales(RM and Instrumentation Center)... RM/Standard Samples R&D and Sales(Proficiency Testing)... Capability Verification and Inter-laboratory Comparison... Customized Training CNAS Consulting and Industry Quality Improvement Services...
Standardization System Construction Transformation of Scientific and Technological Achievements... Scientific Research Project Application and Consultation... Product Formula Restoration and Improvement Digital Upgrading and Transformation of Enterprises... Application for Government Policy Subsidies
Routine Performance Testing... Extreme Environment Testing... Reliability Assessment... Advanced Ceramic Material Testing... Ceramic Matrix Composite Material Testin... Resin-based Composite Material Testing... Carbon-based Composite Materials Testing... Coating Material Testing... High-temperature Metal Material Testing...
- Management System Certification...
- Research Services
Glass Materials Testing... Friction Material Testing... Indoor Environment Testing...
- Management System Certification...
- CCC Certification
- Measurement and Calibration...
- Research Services
- Intelligent Instrumentation...
- Equipment R&D and Manufacturing...
- Operation and Maintenance of Environment...
- Operation and Maintenance of Environment...
- Research Services
Glass Materials Testing... Friction Material Testing... Highway Engineering Testing...
- Management System Certification...
- Research Services
Photovoltaic Products Testing... Glass Materials Testing... Detection Business
- Management System Certification...
- Product Quality Forensic Appraisal...
- Laboratory Construction Services...
- Research Services
- Wind Turbine Blade Testing
Power Testing
- Measurement and Calibration...
Decoration Materials Testing... Building Materials Testing... Engineering Materials Testing... Cement and Primary Combustion Materials ... Building and Sanitary Ceramics Testing... Green Wall Materials Testing... Refractory Materials Testing... Stone Testing Inorganic Chemical Product Testing... Waterproof and Water-saving Materials Te... Wind Turbine Blade Testing... Fiberglass Product Testing... Cement Concrete Product Testing... Detection Business Construction Engineering Testing... Highway Engineering Testing... Civil Air Defense Engineering Testing... Water Conservancy Project Testing... Nuclear Power Engineering Testing... Indoor Environment Testing...
- Management System Certification...
- CCC Certification
- China Promotes Voluntary Product Certifi...
- Voluntary Product Certification for Inst...
- Service Certification...
- Measurement and Calibration...
- Building Engineering Forensic Appraisal...
- Product Quality Forensic Appraisal...
- Safety Technical Services...
- Environmental Protection Technology Serv...
- Education and Training...
- Informatization and Intelligent Construc...
- Energy Efficiency Evaluation...
- Fire Safety Field
- Laboratory Construction Services...
- Research Services
Cement and Primary Combustion Materials ... Cement Concrete Product Testing... Detection Business Nuclear Power Engineering Testing...
- Management System Certification...
- Equipment R&D and Manufacturing...
- Product Quality Forensic Appraisal...
- Safety Technical Services...
- Environmental Protection Technology Serv...
- Education and Training...
- Informatization and Intelligent Construc...
- Energy Efficiency Evaluation...
- Fire Safety Field
- Laboratory Construction Services...
- Quality Improvement Service...
- Research Services
Building and Sanitary Ceramics Testing... Refractory Materials Testing... Glass Materials Testing... Detection Business
- Management System Certification...
- Equipment R&D and Manufacturing...
- Product Quality Forensic Appraisal...
- Safety Technical Services...
- Environmental Protection Technology Serv...
- Education and Training...
- Informatization and Intelligent Construc...
- Energy Efficiency Evaluation...
- Fire Safety Field
- Laboratory Construction Services...
- Research Services
Water Conservancy Project Testing...
- Management System Certification...
- Smart Water Conservancy...
- Research Services
Friction Material Testing... Special Equipment Testing...
- Management System Certification...
- Research Services
Non-metallic Sealing Products Testing... Non-metallic Mineral Products Testing... Coal Testing
- Management System Certification...
- Product Quality Forensic Appraisal...
Fiber Reinforced Plastics Product Testin... Friction Material Testing...
- Management System Certification...
- China Promotes Voluntary Product Certifi...
- Voluntary Product Certification for Inst...
- Carbon-related Certification...
- Services to Tackle Climate Change...
- Green Manufacturing System Service...
- Life Cycle Assessment LCA Services...
- Management Services for Energy and Envir...
- International Project Services...
- Smart Environmental Protection...
- Environmental Protection Technology Serv...
- Ecological Environment Consulting...
Construction Engineering Testing... Civil Air Defense Engineering Testing... Ecological Environment, Health and Safet... Indoor Environment Testing... Food Safety and Agricultural Consulting...
- Management System Certification...
- Life Cycle Assessment LCA Services...
- Management Services for Energy and Envir...
- Equipment R&D and Manufacturing...
- Operation and Maintenance of Environment...
- Measurement and Calibration...
- Environmental Damage Forensic Appraisal...
- Public Security Drug Testing...
- Smart Environmental Protection...
- Safety Technical Services...
- Operation and Maintenance of Environment...
- Ecological Environment Consulting...
- Project and Fund Application...
- Education and Training...
- Informatization and Intelligent Construc...
- Energy Efficiency Evaluation...
- Fire Safety Field
Textile Testing Non-metallic Mineral Products Testing... Indoor Environment Testing...
- Management System Certification...
- Measurement and Calibration...
Ecological Environment, Health and Safet... Food Safety and Agricultural Consulting...
- Management System Certification...
- Research Services
- Smart Water Conservancy...
- Smart Agriculture
- Smart Environmental Protection...
- Informatization and Intelligent Construc...
- Photovoltaic Products Testing
- Glass Materials Testing
- Friction Material Testing
- Standardization System Development
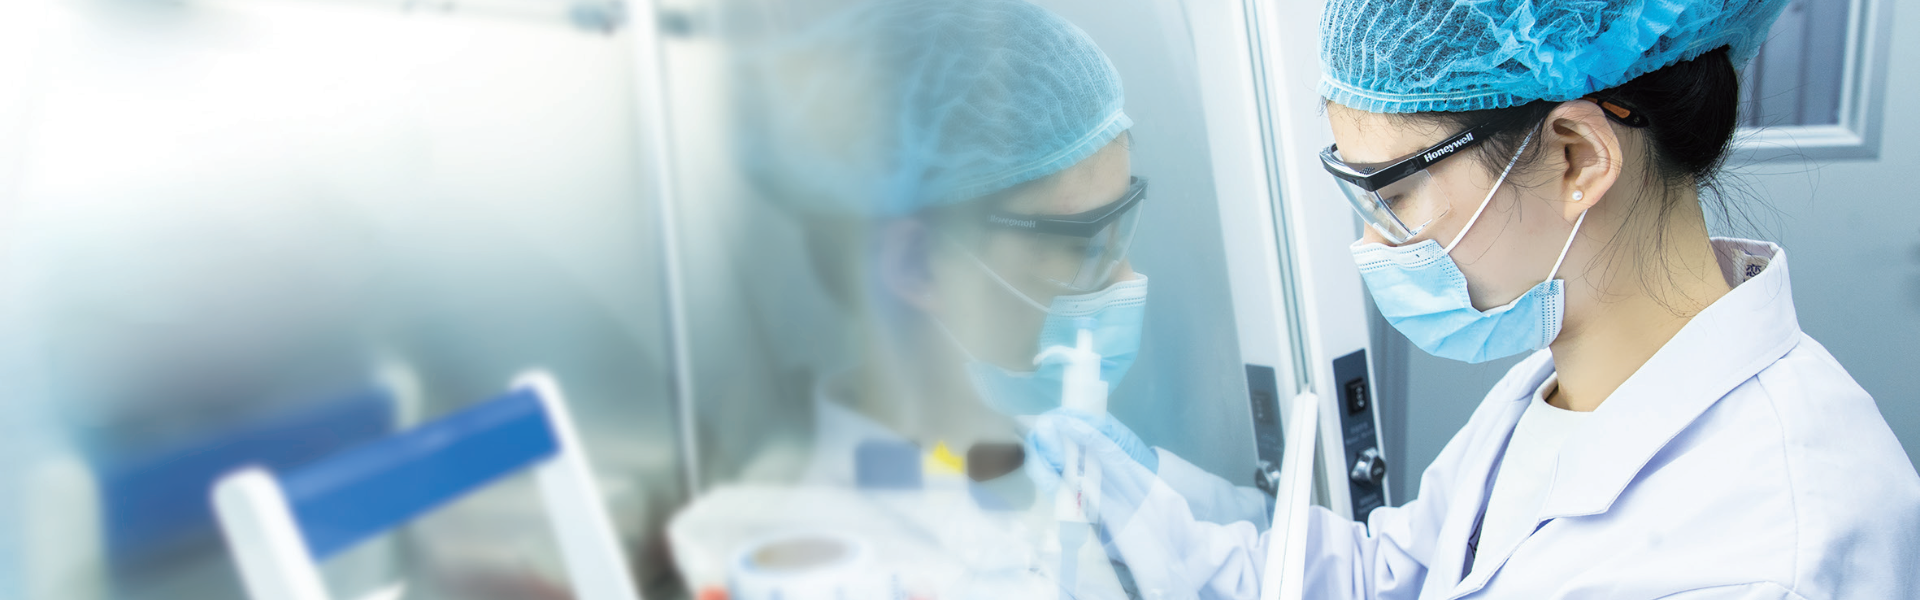
In the field of chemical analysis in the cement industry, efficiency, accuracy, and intelligence have always been the focus of industry attention. Traditional wet chemical analysis methods are time-consuming, the X-ray fluorescence (XRF) pressed powder method has limited accuracy and precision, and the traditional XRF fused bead method imposes overly stringent requirements on experimental operations. To address these challenges, the technical expert team of China Testing & Certification International Group Co., Ltd. has conducted in-depth research, breaking through multiple technical barriers in XRF detection, and successfully developed a detection technology based on X-ray fluorescence spectrometry — MLD Technology. With XRF technology as its core, it creates an optimized testing solution.
MLD Technology is a groundbreaking fusion testing technology developed based on X-ray fluorescence spectrometry (XRF). It breaks the shackles of traditional chemical analysis methods and builds an innovative solution for XRF applications in the cement testing field, providing an efficient, convenient, cost-effective, and environmentally friendly full-process solution for the testing of cement and raw material samples.
Service Contents
Provide customized solutions for the accurate chemical composition analysis of samples such as cement, raw meal, clinker, gypsum, limestone, slag; siliceous raw materials, ferrous raw materials, aluminous raw materials, as well as various industrial waste slag samples including sulfuric acid slag and non-ferrous metal ash slag.
Analysis Elements
Silicon Dioxide (SiO₂)
Aluminum Oxide (Al₂O₃)
Iron Oxide (Fe₂O₃)
Titanium Dioxide (TiO₂)
Calcium Oxide (CaO)
Magnesium Oxide (MgO)
Sulfur Trioxide (SO₃)
Potassium Oxide (K₂O)
Sodium Oxide (Na₂O)
Manganese Oxide (MnO)
Phosphorus Pentoxide (P₂O₅)
Chromium Trioxide (Cr₂O₃)
Zinc Oxide (ZnO)
Chloride Ion (Cl⁻)
Service Standards
Cement: Common Portland cement, oil well cement, moderate and low heat cement, masonry cement, raw meal, clinker — GB/T 176
Aluminate Cement: Aluminate cement — GB/T 205
Limestone: Limestone for building materials, quicklime, hydrated lime — GB/T 5762
Ferrous Raw Materials: Iron ore, sulfuric acid slag, non-ferrous metal ash slag, converter slag, iron tailings, etc. — JC/T 850
Siliceous Raw Materials: Sandstone, clay, shale — JC/T 874
Aluminous Raw Materials: Fly ash, coal gangue — GB/T 176
Slag: Granulated blast furnace slag / slag powder — GB/T 27975
Technical Advantages
1. High Efficiency: Complete analysis of 80 samples per day, achieving a 20 to 40 times increase in efficiency compared to traditional chemical analysis (2-4 samples per day).
2. Low Technical Threshold: No professional or experience requirements; ordinary personnel can operate after one day of training, significantly reducing skill requirements for labor.
3. Cost Optimization: Taking a single 5,000 tons/day production line as an example, it can reduce the need for two fixed positions.
4. Environmental Friendliness: No use of strong acids or alkalis throughout the entire process, eliminating waste liquid and gas emissions at the source, while simultaneously reducing environmental treatment costs.
Links
- About CTC
-
Our Services
- Our Services
-
By Industry
Building Materials and Construction Engineering Food and Agricultural Products Intelligent Manufacturing Rail Traffic Cement and Cement Products New Materials Photovoltaic Glass Automobile and Parts Special Equipment Water Resources Electrical Engineering Environment and Safety Low-carbon Environmental Protection and Green Certification Cosmetics and Daily Chemicals Geology and Mineral Resources Digital Services
- News Center